Source the Right Fabric for Every Custom Apparel Project
From fibre composition and construction to weight, finish and brand positioning -- we help you select and verify materials that match your product, market and production requirements.
Select Fabric Around Your Brand Positioning
The right fabric decision starts with the brand story, not the swatch book. Different target markets, price points and product categories call for different fibre, construction and finish combinations.
Premium / Luxury Streetwear
Heavyweight 400-500 GSM French Terry or brushed fleece. Tight knit structure, dense face, minimal pilling. Supports premium embroidery and tonal branding.
High-end BrandMid-Market Fashion Brand
280-360 GSM cotton-poly blends balance cost and quality. Comfortable hand feel, consistent colour response, suitable for screen print and DTF decoration.
Commercial VolumeAthletic / Performance Label
Technical polyester or cotton-polyester with moisture management, stretch and quick-dry properties. Four-way stretch for fitted tracksuits and active hoodies.
Performance FocusSustainable / Eco Brand
Organic cotton (GOTS-certified), recycled polyester (GRS) or TENCEL™ blends. Verified fibre sourcing documentation available upon request.
Eco-ConsciousPrivate Label / Wholesale
Consistent construction and colour repeatability across large orders. Stock fabric options allow faster lead times for replenishment programmes.
High VolumeExport / International Buyer
EN, REACH and CPSC compliance documentation. Accurate fibre labelling, care instruction content and test report coordination for EU and US markets.
Compliance-ReadyFabric Composition & Performance Classification
Understanding fibre composition, knit construction and finishing treatment helps define the final garment's durability, comfort, weight and decoration compatibility.
100% Cotton -- Combed Ring Spun
Best for premium T-shirts and heavyweight hoodies. Pre-shrunk treatment reduces post-wash dimensional change.
Organic Cotton (GOTS)
Traceable supply chain and certification documentation available. Suitable for eco-positioned brands.
French Terry / Loopback
Smooth face with looped interior. Standard for hoodies and sweatshirts. GSM range 280-450.
100% Polyester -- Jersey
Ideal for sublimation printing and performance tracksuits. Low cost, high colour saturation.
Recycled Polyester (rPET)
GRS certification available. Positions performance garments within sustainability narratives.
Polar Fleece / Sherpa
Popular for winter hoodies, outerwear linings and streetwear layering pieces.
80% Cotton / 20% Polyester
Most common blend for casual hoodies and T-shirts. Balances natural feel with improved shape retention.
Tri-Blend (CVC)
Cotton, polyester and rayon blend. Vintage-feel drape. Popular for fashion-forward T-shirt programmes.
Cotton / Spandex (95/5)
Fitted T-shirts, bodycon joggers and slim-cut tracksuits. Stretch improves comfort without losing shape.
Single Jersey
Standard T-shirt construction. Lightweight at 120-200 GSM, medium at 200-280 GSM.
Double Jersey (Interlock)
Both faces identical. No curling on edges. Preferred for polo shirts and structured knitwear.
Waffle / Textured Knit
Distinctive surface texture adds product differentiation. Popular for casual loungewear and streetwear base layers.
Weight, Colour, Hand-feel & Functional Selection
Each specification dimension affects cost, lead time, decoration performance and how the finished garment is perceived by the end consumer.
Fabric Weight (GSM)
Heavier GSM generally increases warmth, structure and perceived quality. It also increases shipping cost per unit. The right weight is determined by silhouette, season and brand positioning.
Colour Direction
Colour accuracy depends on fibre type and dye process. We recommend physical lab dip or Pantone reference confirmation before bulk production dyeing begins.
Hand Feel & Surface Finish
Describe your preferred hand feel using reference garments or brand analogues. We develop swatch sets for physical review before production commitment.
Functional Performance
Fabric Swatch & Sampling Verification
Physical verification of fabric before bulk production avoids colour, weight and hand-feel discrepancies that are difficult to resolve after cutting.
Brief & Reference Collection
Collect fabric name, composition, GSM target, colour direction (Pantone / physical sample), construction preference and decoration method from the client.
InputFabric Sourcing & Swatch Preparation
Identify candidate fabrics from verified mills. Prepare physical swatch sets with composition label, GSM, construction note and suggested application.
SourcingSwatch Submission & Client Review
Physical swatches or high-resolution digital reference images shared for client review. Comments collected on colour, weight, texture and surface finish.
ReviewLab Dip / Strike-off Approval
Colour lab dip submitted for Pantone or reference colour matching. Print strike-off verified for colour accuracy, detail and wash fastness before fabric bulk order.
Colour ApprovalSample Garment Fabric Confirmation
First sample produced in approved fabric. GSM, composition, colour, hand feel and shrinkage measured against brief. Sign-off required before bulk cutting.
Garment SampleBulk Fabric Inspection
Incoming fabric checked for weight, colour consistency, width, defect rate and wash shrinkage against approved standard before cutting begins.
Quality Control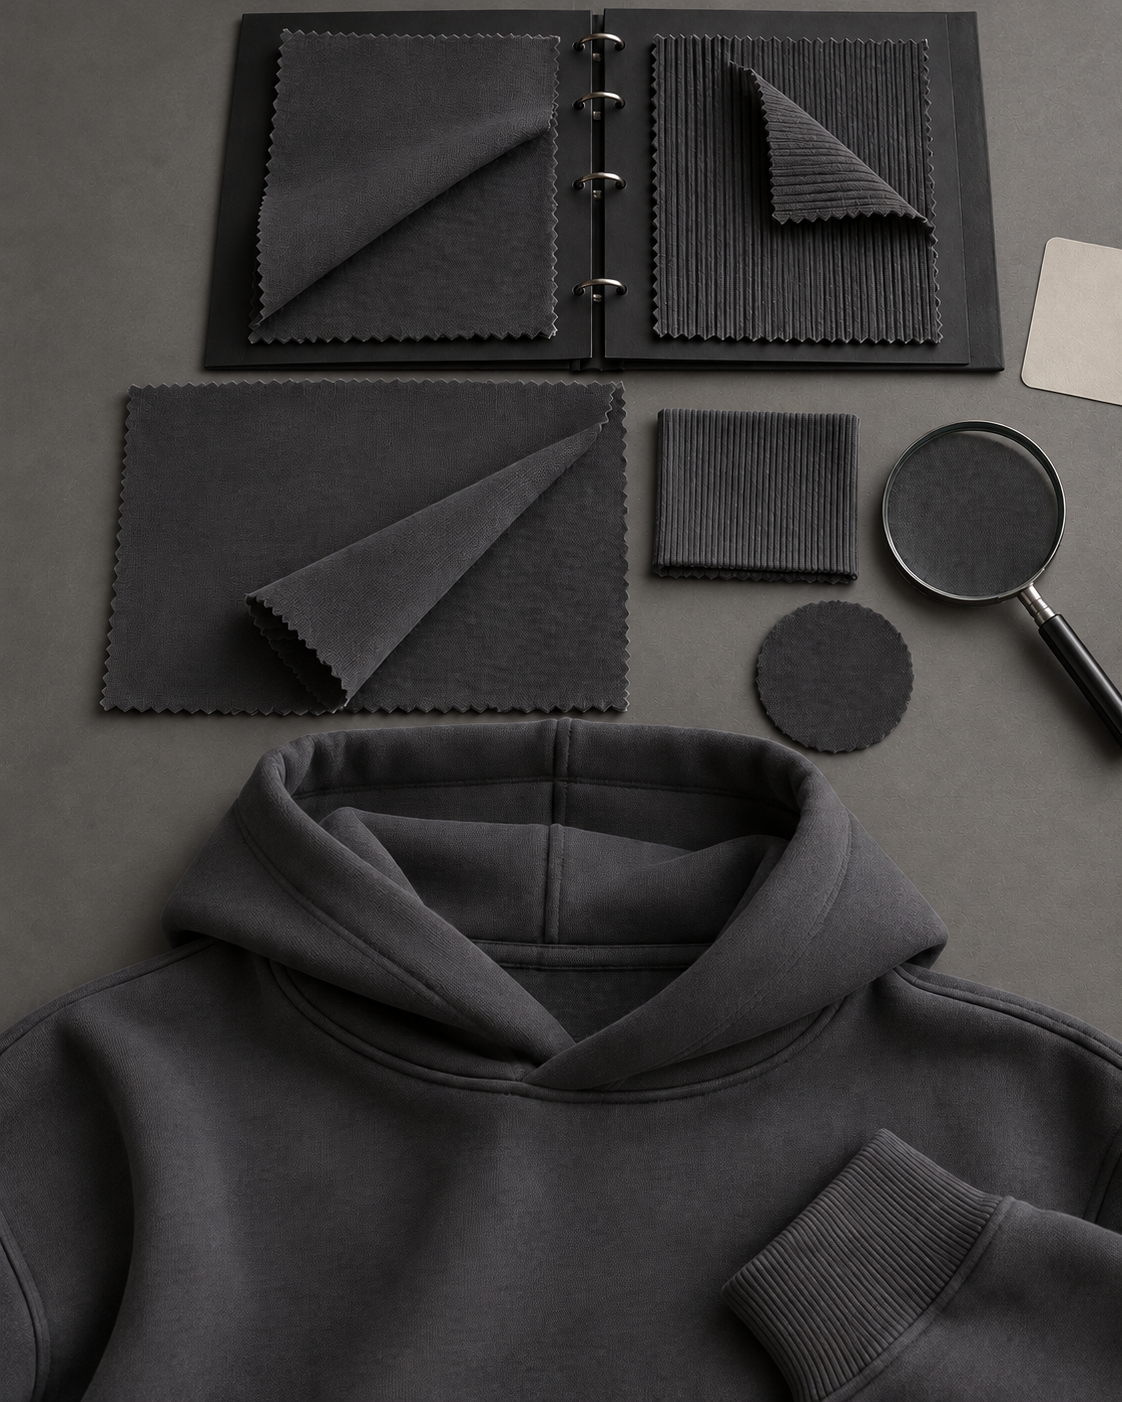
Fabric Cost, MOQ & Lead-time Impact
Fabric choice is the single largest variable in garment unit cost and production timeline. Understanding the relationship between fibre, construction and order quantity helps set realistic budgets and delivery expectations.
| Fabric Type | Typical GSM | Cost Range | Minimum Yardage | Lead Time (Sample) | Lead Time (Bulk) |
|---|---|---|---|---|---|
| 100% Cotton Jersey | 160-280 GSM | Lower-Mid | 200-500 yds | 7-14 days | 25-40 days |
| Combed Ring Spun Cotton | 180-260 GSM | Mid | 300-600 yds | 10-18 days | 30-45 days |
| French Terry / Loopback | 280-420 GSM | Mid-High | 500-800 yds | 12-20 days | 35-50 days |
| Heavyweight Fleece | 380-500 GSM | Mid-High | 500-1,000 yds | 14-22 days | 40-55 days |
| Cotton/Poly Blend | 200-350 GSM | Lower-Mid | 200-400 yds | 7-14 days | 25-40 days |
| Organic Cotton (GOTS) | 160-300 GSM | High | 500-1,000 yds | 14-25 days | 40-60 days |
| Performance Polyester | 130-200 GSM | Lower | 200-400 yds | 7-12 days | 20-35 days |
| Custom Dye / Special Finish | Varies | High (+ dye cost) | 800-1,500 yds | 18-30 days | 45-65 days |
Fibre & Certification
Organic certification and specialty fibres (TENCEL™, rPET) add 15-40% to raw material cost. Plan certification lead time alongside production scheduling.
Custom Colour & Construction
Custom dye requires minimum yardage per colour. Sharing a dye lot across multiple SKUs can reduce per-unit cost. Stock colours eliminate dye lead time.
Mill Location & Stock Status
In-stock greige fabric plus local dyeing can reduce fabric lead time significantly. Imported mill fabrics or custom constructions add 3-6 weeks before cutting.
Fabric Pairing Recommendations by Product Category
Each product category has structural and functional requirements that influence the optimal fabric choice. The following recommendations are starting points -- every project is confirmed through sample review.
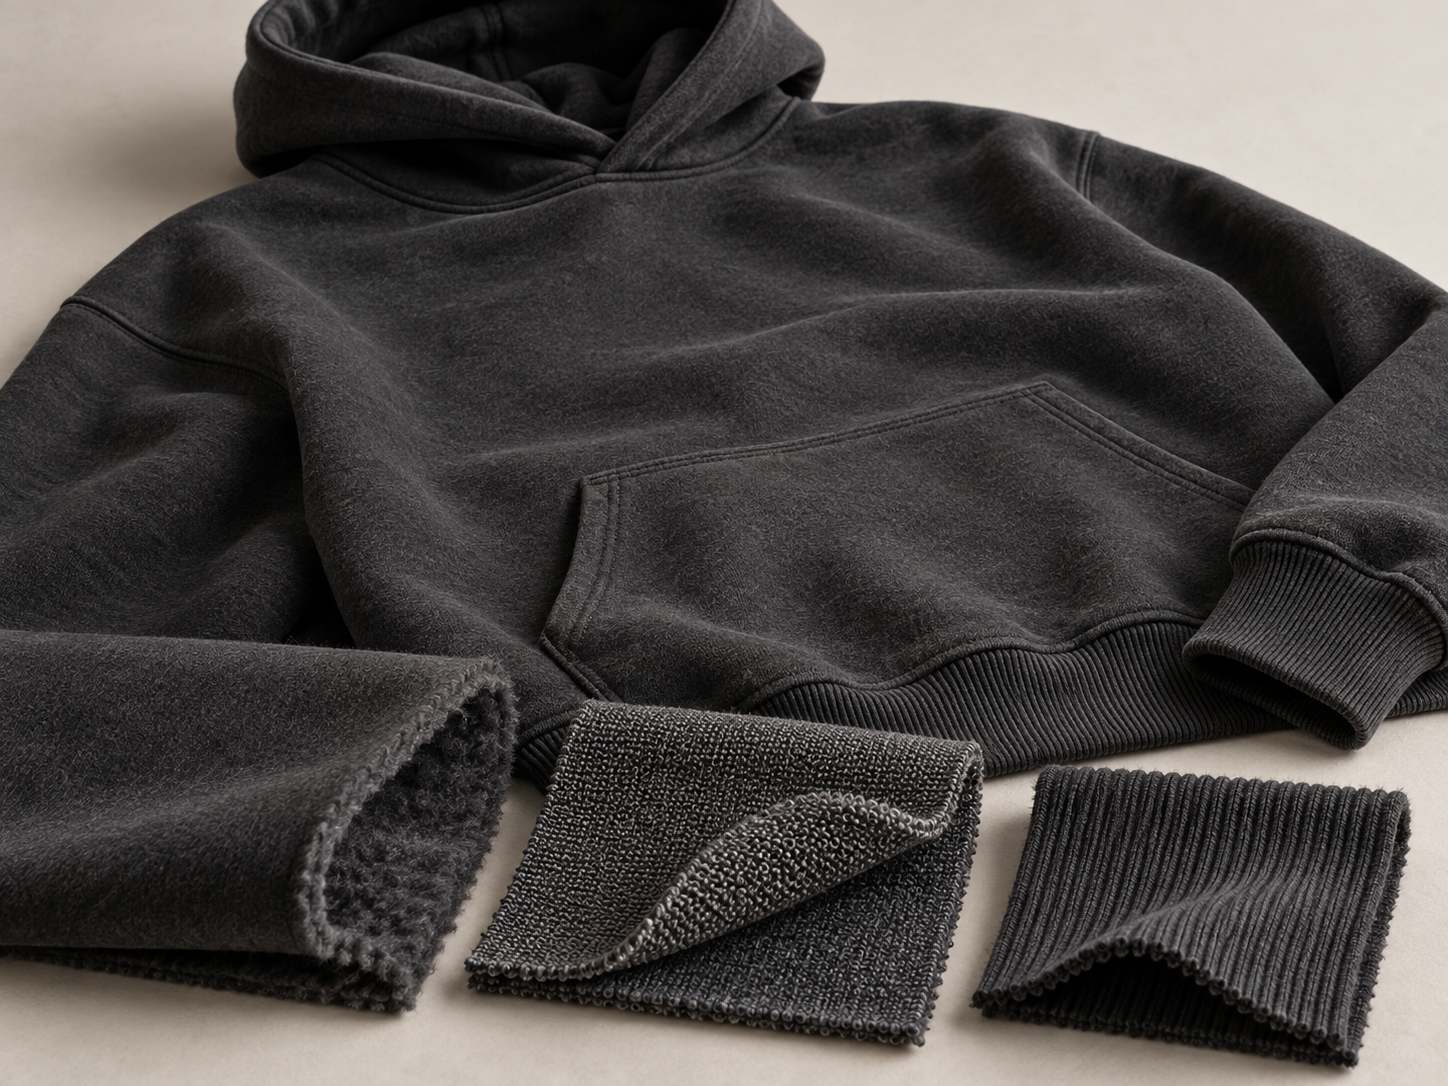
Custom Hoodies
Pullover & Zip-up Hoodies
French Terry or loopback fleece 280-420 GSM for standard fits. Heavyweight 400-500 GSM brushed fleece for premium streetwear. Ribbed cuffs and hem in matching composition.
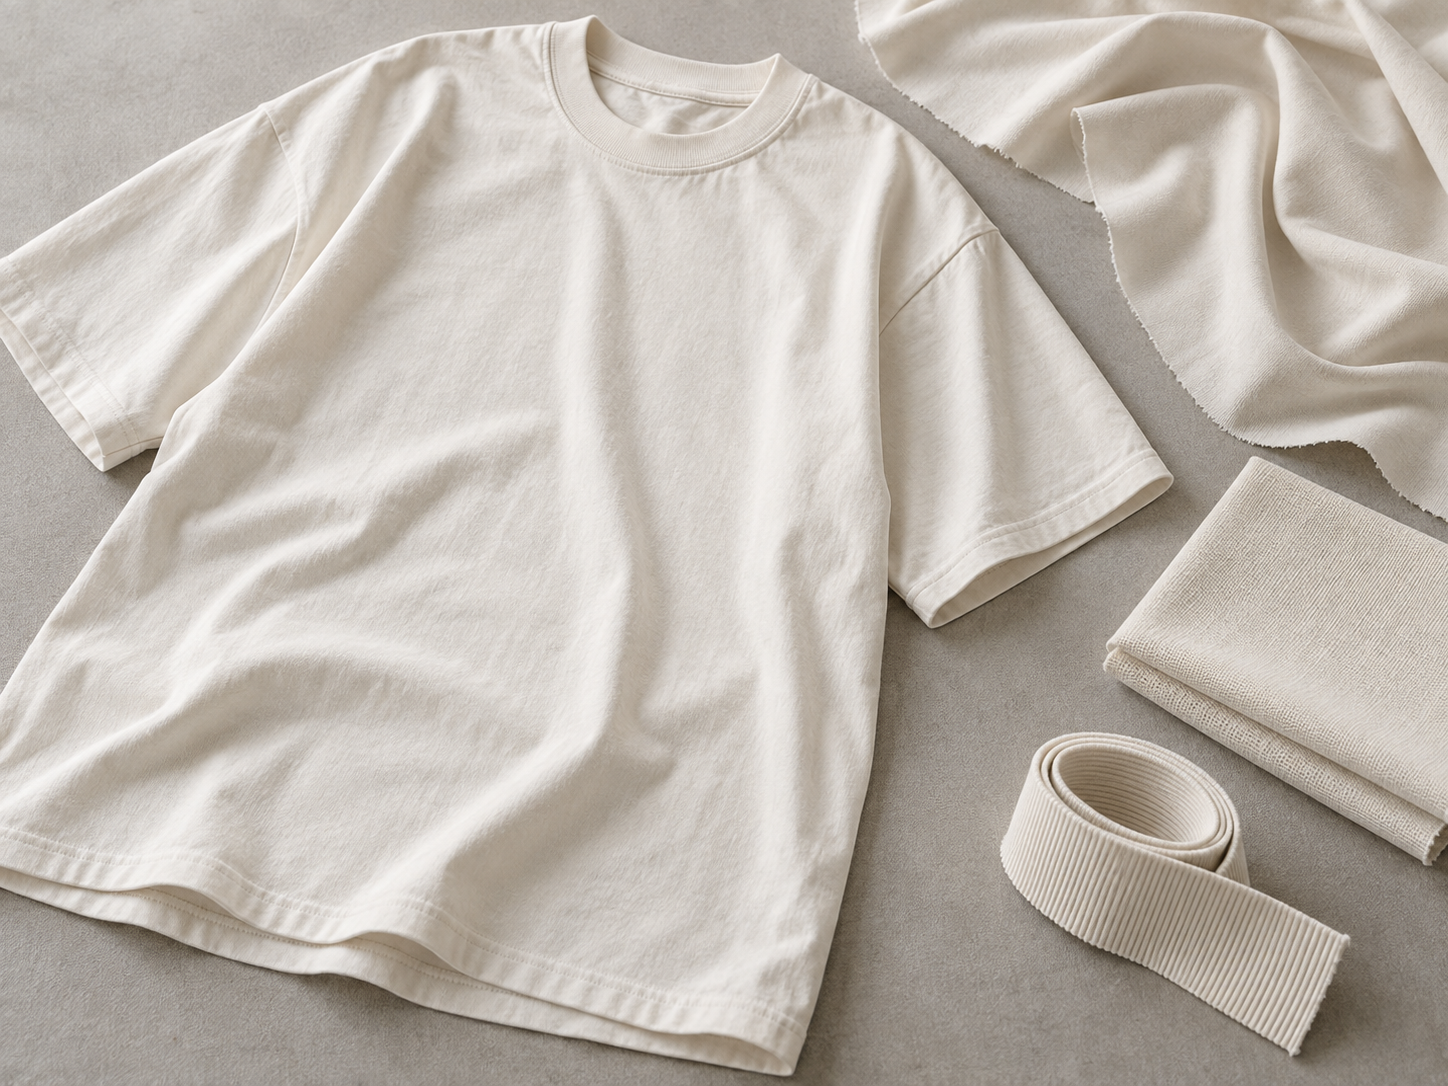
Custom T-Shirts
Regular, Oversized & Drop Shoulder
180-220 GSM combed cotton for standard retail. 250-320 GSM for heavyweight streetwear tees. Oversized and drop-shoulder silhouettes benefit from mid-weight single jersey.
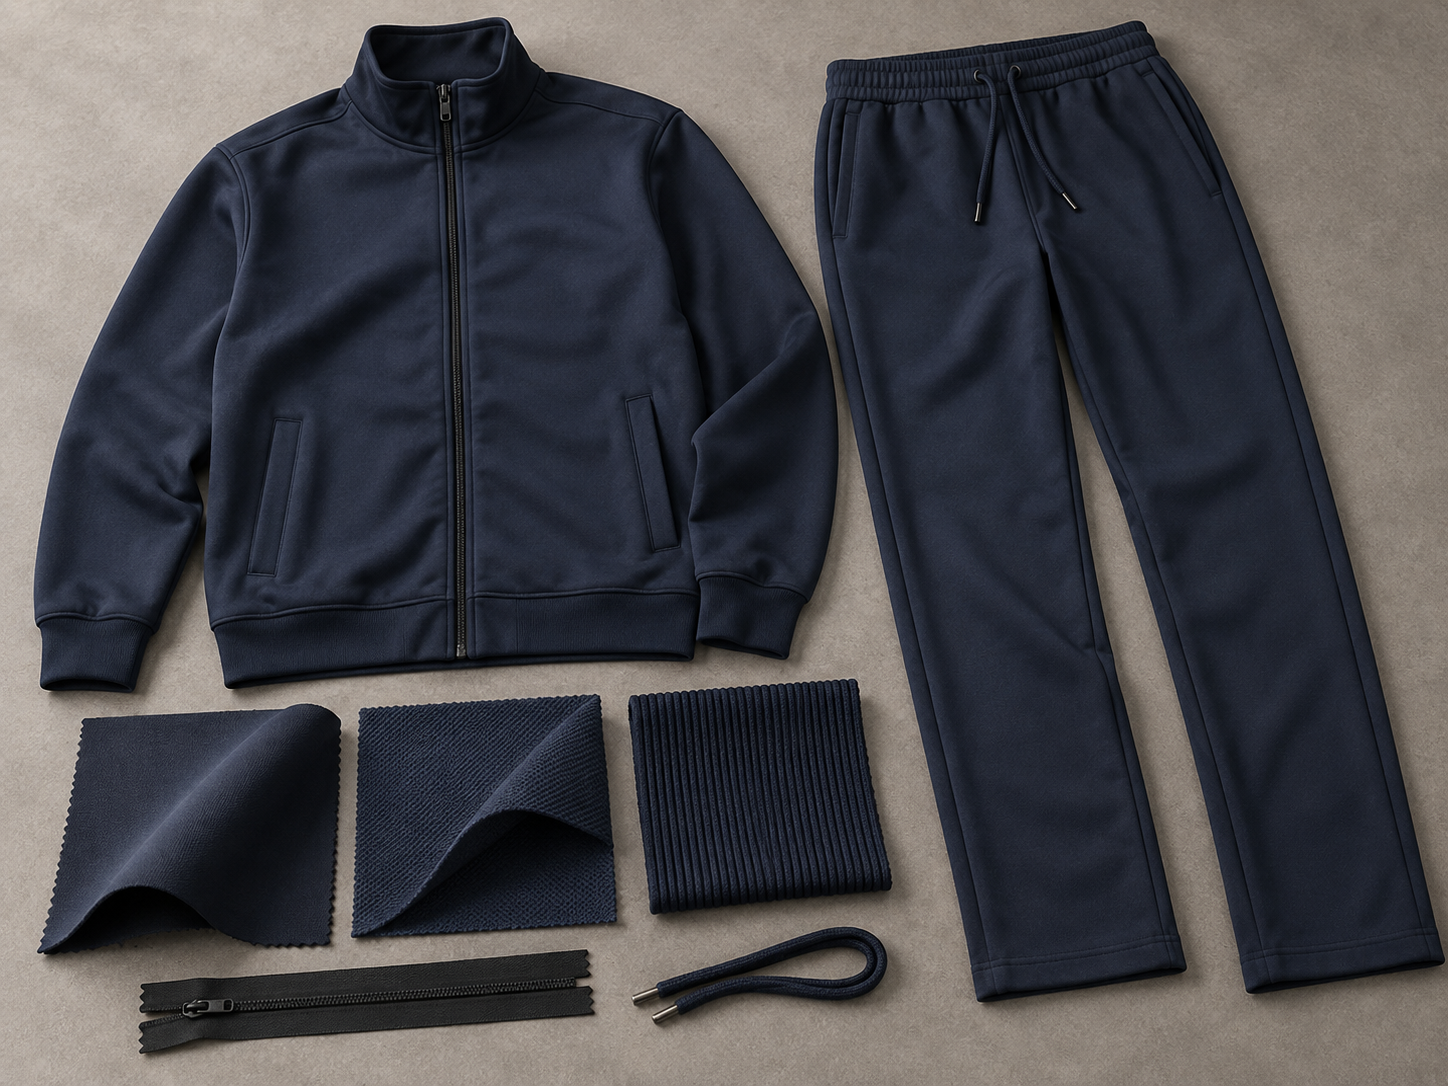
Custom Tracksuits
Athletic, Casual & Streetwear Sets
Performance polyester or cotton-poly for athletic cuts. French Terry or fleece sets for casual and streetwear. Matching top and bottom fabric from same dye lot for colour consistency.
| Decoration Method | Recommended Fabric Surface | Avoid | Notes |
|---|---|---|---|
| Screen Print | Smooth single jersey, combed cotton | High-stretch or heavily textured knits | Confirm base colour and pre-treat dark garments |
| DTF Transfer | Cotton or cotton-blend jersey | 100% nylon or heavily coated surfaces | Wash fastness testing recommended |
| Embroidery | Stable knit, French Terry, fleece | Very lightweight or high-stretch single jersey | Backing material selection affects final result |
| Sublimation | 100% polyester only | Any cotton-containing fabric | Colour vibrancy directly linked to polyester content |
| Puff / Foil Print | Smooth jersey, tight construction | Heavily brushed or pile surfaces | Test adhesion on sample before bulk commitment |
Project Inquiry Form
The more detail you provide, the faster we can prepare a structured cost and timeline estimate.